Custom MOCVD Epi Wafers and III-V Layer Structures
Metal Organic Chemical Vapor Deposition (MOCVD) is used to grow custom
III-V semiconductor epitaxial structures
for photodetectors, laser diodes, LEDs, high-speed electronics, solar cells, RF devices, and photonic integrated circuits.
UniversityWafer can help researchers source custom epi wafers with controlled substrate type, layer sequence, alloy composition, thickness, doping, and cap-layer specifications. Common material systems include
InGaAs,
InP,
GaAs,
AlGaAs, InGaP, InAlAs, GaN, and AlGaN.
Custom InGaAs PIN Epi Wafer Request
A physics PhD researcher requested a custom InGaAs PIN epi structure grown on an InP substrate:
I would like to ask whether your company has PIN InGaAs epi wafers or can produce a custom PIN InGaAs epi wafer.
Requested layer structure:
- n+ InP substrate, (100) orientation, requested thickness of 100 µm
- n+ InP buffer layer, 1 µm
- n− In0.53Ga0.47As absorption layer, 3–4 µm
- n− InP cap layer
The exact dopant species and doping concentration are not the primary concerns for this application.
Request a Custom MOCVD Epi Wafer Quote
Send us your complete layer structure, substrate requirements, target doping, and quantity. The more information you provide, the faster we can evaluate manufacturability and prepare pricing.
Get Your Custom Epi Wafer Quote FAST! Or,
Buy Online and Start Researching Today!
Recommended InGaAs/InP Epi Configuration
UniversityWafer, Inc. replied: The proposed InGaAs/InP structure can be considered for custom MOCVD growth. For this type of project, a standard
InP substrate
would typically be approximately 2 inches in diameter and about 350 µm thick rather than 100 µm.
The substrate may be specified as n-type, p-type, or semi-insulating depending on the required electrical isolation, contact design, and final device architecture.
A thin InP cap layer, such as approximately 0.1 µm, may be suitable for surface protection, contact formation, or device processing. The final cap thickness and doping should be selected according to the intended photodiode, detector, transistor, or optical-device design.
Custom InGaAs/InP epi wafers may be used for:
Reference #254358 for specifications and pricing.
MOCVD Epitaxial Growth Capabilities
UniversityWafer works with custom
MOCVD epitaxy
capabilities for compound-semiconductor structures with controlled thickness, composition, conductivity, carrier concentration, and surface quality.
Available project types may include:
- InGaAs layers on InP substrates
- InP buffer, cap, and window layers
- GaAs and AlGaAs heterostructures
- InGaP and InAlAs alloy layers
- PIN and avalanche photodiode structures
- Quantum wells and barrier layers
- Laser diode and LED epi wafers
- HEMT and high-frequency transistor structures
- GaN and AlGaN wide-bandgap structures
- Multi-junction solar-cell epitaxy
Specifications to Include with Your Epi Wafer Request
- Substrate material: InP, GaAs, sapphire, SiC, silicon, or another platform
- Wafer diameter and thickness
- Crystal orientation and offcut
- Conductivity type: n-type, p-type, or semi-insulating
- Complete layer sequence from the substrate to the top surface
- Thickness of each layer
- Alloy composition and any grading requirements
- Dopant species and target concentration
- Cap, contact, window, or passivation layer
- Surface finish and backside requirements
- Quantity and acceptable tolerances
Pricing and lead time depend on wafer diameter, substrate availability, material system, layer count, total epi thickness, doping requirements, characterization, and order quantity.
What Is Metal Organic Chemical Vapor Deposition?
Metal Organic Chemical Vapor Deposition (MOCVD), also called
Metalorganic Vapor-Phase Epitaxy (MOVPE), is a semiconductor epitaxy process used to grow
high-quality crystalline layers on heated wafers. It is especially important for
III-V semiconductor materials,
including GaAs, InP, GaN, AlGaAs, InGaAs, AlGaN, and related compound-semiconductor systems.
During MOCVD growth, metal-organic source compounds and hydride gases are introduced into a controlled
reaction chamber. The precursors transport the required elements to the wafer surface, where they react
or decompose to form an epitaxial film. By adjusting temperature, pressure, gas flow, precursor ratios,
and dopant sources, engineers can control layer thickness, composition, doping, and interface quality.
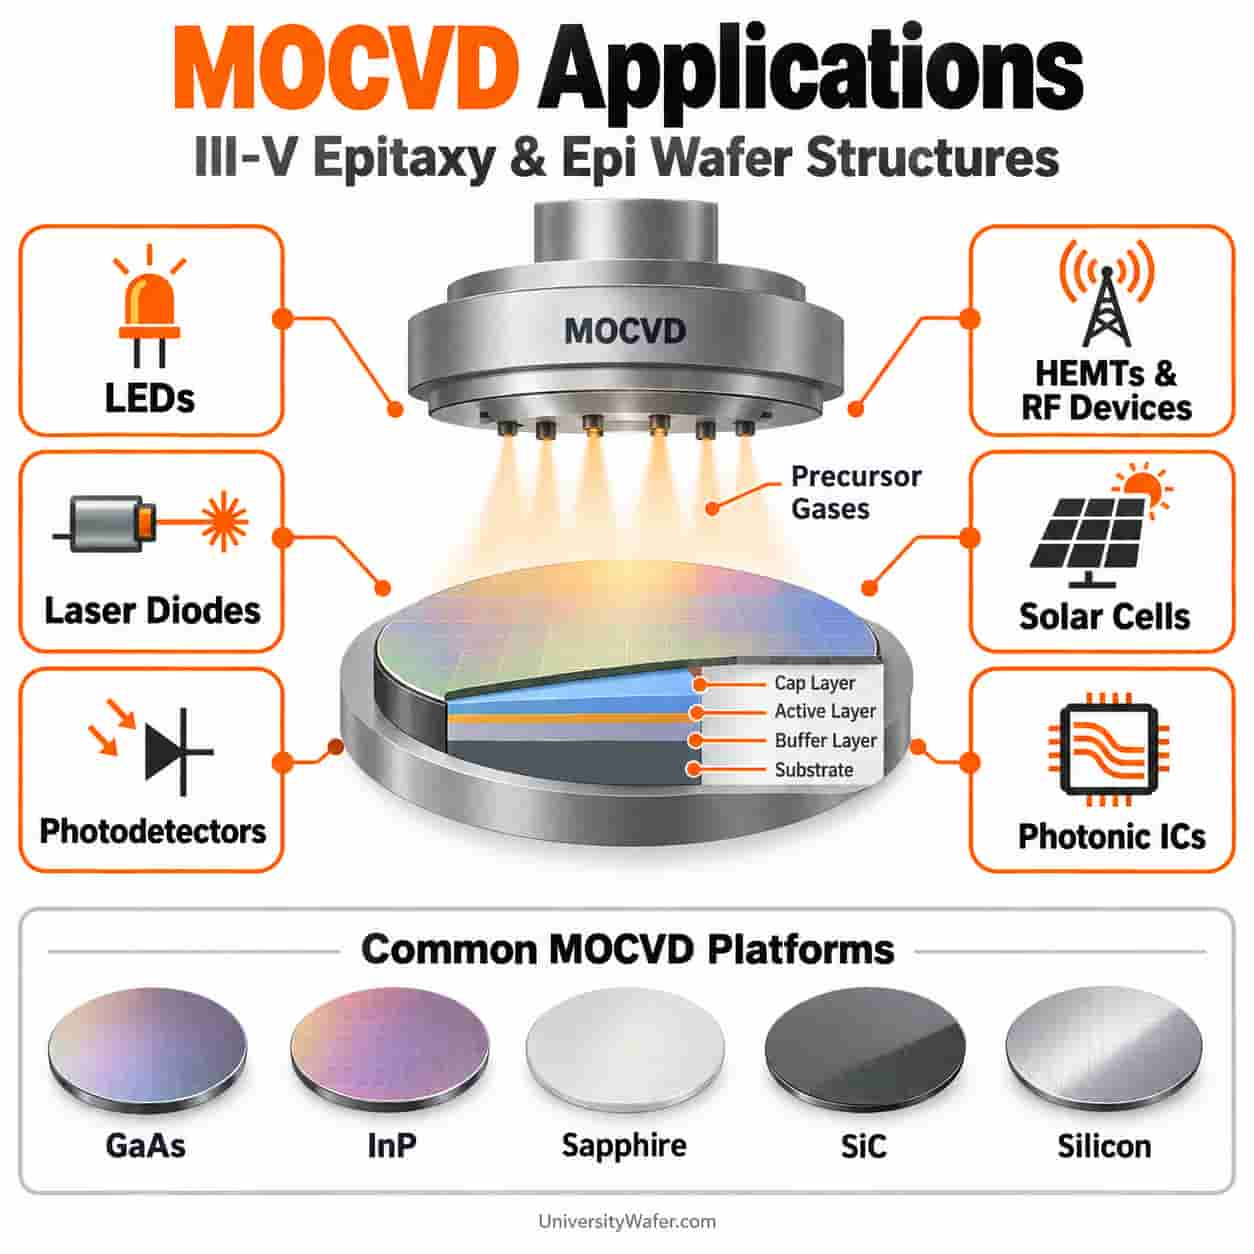
MOCVD is widely used to fabricate LEDs, laser diodes, photodetectors, solar cells, high-electron-mobility
transistors, RF devices, and photonic integrated circuits.
MOCVD Substrates and Material Systems
The substrate must provide suitable crystal orientation, surface quality, thermal stability, and lattice
compatibility for the intended epitaxial structure. Common MOCVD platforms include:
-
Gallium Arsenide (GaAs)
for AlGaAs, InGaP, InGaAs, lasers, solar cells, and high-frequency electronics
-
Indium Phosphide (InP)
for InGaAs, InAlAs, photodetectors, optical communications, and high-speed devices
-
Sapphire and GaN-on-sapphire
for GaN and AlGaN LED, RF, and power-device structures
-
Silicon Carbide (SiC)
for GaN epitaxy, high-power electronics, and high-temperature devices
-
Silicon
for selected GaN-on-Si, photonic, and heterogeneous-integration processes
InGaAs is commonly grown as an
epitaxial alloy layer on InP, GaAs, or another engineered buffer structure rather than being used as the
primary bulk substrate in most MOCVD processes.
Main Advantages of MOCVD
-
Precise Layer-Thickness Control
MOCVD can grow thin epitaxial layers, quantum wells, barriers, cap layers, and multilayer stacks with
tightly controlled thicknesses.
-
Controlled Alloy Composition
Adjusting precursor flow ratios allows engineers to tune the composition and bandgap of ternary and
quaternary compounds such as AlGaAs, InGaAs, InGaP, and AlGaN.
-
Accurate Doping Profiles
Dopant gases can be introduced during growth to create n-type, p-type, graded, delta-doped, and
modulation-doped layers.
-
High-Quality Epitaxial Interfaces
MOCVD can produce abrupt interfaces and low-defect crystalline layers when the substrate, chamber,
and process conditions are properly optimized.
-
Complex Heterostructure Growth
The process supports quantum wells, superlattices, distributed Bragg reflectors, HEMT structures,
PIN photodiodes, laser structures, and multi-junction solar-cell stacks.
-
Large-Wafer and Multi-Wafer Processing
Commercial reactors can process multiple wafers per run and are compatible with high-volume LED,
RF, power, and optoelectronic manufacturing.
-
Broad Compound-Semiconductor Compatibility
MOCVD is suitable for arsenides, phosphides, nitrides, and other compound-semiconductor families used
across electronics and photonics.
-
Good Repeatability
Modern reactors use controlled gas delivery, temperature monitoring, and in-situ diagnostics to
improve run-to-run and wafer-to-wafer consistency.
Main Disadvantages of MOCVD
-
Hazardous Precursors
Arsine, phosphine, ammonia, hydrogen, and many metal-organic compounds require specialized storage,
gas cabinets, monitoring systems, exhaust treatment, and trained personnel.
-
High Capital and Operating Costs
MOCVD reactors, abatement systems, gas-delivery equipment, maintenance, and high-purity precursors can
be expensive.
-
Complex Process Development
Film quality depends on many interacting variables, including wafer temperature, chamber pressure,
precursor chemistry, carrier-gas flow, rotation speed, and reactor geometry.
-
Possible Carbon or Oxygen Incorporation
Metal-organic chemistry and background contamination can introduce unwanted impurities if growth
conditions and chamber cleanliness are not carefully controlled.
-
High Growth Temperatures
Many epitaxial processes require elevated temperatures that may be incompatible with completed devices,
temperature-sensitive films, or certain bonding materials.
-
Precursor Utilization and Waste
Only part of the supplied precursor may contribute to film growth, increasing material cost and placing
additional demands on exhaust and abatement systems.
-
Wafer Uniformity Challenges
Thickness, composition, and doping uniformity must be carefully controlled across larger wafers and
multi-wafer reactor loads.
-
Maintenance and Chamber Conditioning
Deposits can form on reactor components, requiring cleaning, replacement, and chamber-conditioning
procedures to maintain reproducible growth.
MOCVD Advantages and Disadvantages at a Glance
| Advantages |
Disadvantages |
| Precise thickness and composition control |
Expensive reactor and gas-delivery equipment |
| Accurate in-situ doping |
Toxic, pyrophoric, or corrosive precursors |
| Complex heterostructure growth |
Complex process optimization |
| High crystalline quality |
Possible carbon, oxygen, and background contamination |
| Scalable multi-wafer manufacturing |
High operating and maintenance costs |
| Compatible with many III-V materials |
Elevated growth temperatures |
When Is MOCVD Better Than MBE?
MOCVD growth is often preferred when manufacturers need repeatable, high-throughput growth across production wafers—for example, AlGaN/GaN HEMT epitaxy, InGaN LED structures, or multi-junction photovoltaic layers. MBE can be attractive for small-batch research requiring precise flux control and in-situ ultra-high-vacuum surface diagnostics. Neither technique is universally superior: compare film requirements, wafer size, precursor availability, development effort, and expected production volume.
What Affects MOCVD Epitaxial Film Quality?
For GaAs wafers, InP substrates, and SiC substrates, the resulting epitaxial quality depends on substrate orientation, surface preparation, lattice mismatch, precursor chemistry, temperature uniformity, and wafer bow. Bandgap engineering also depends on accurately controlling alloy composition in heterostructures. The appropriate acceptance criteria may include thickness uniformity, carrier concentration, crystal quality, and defect density.
MOCVD Compared with Molecular Beam Epitaxy
MOCVD and molecular beam epitaxy (MBE) are both used to grow high-quality compound-semiconductor layers,
but they are optimized for different priorities.
| Feature |
MOCVD |
MBE |
| Growth environment |
Controlled-pressure gas-phase reactor |
Ultra-high-vacuum chamber |
| Source materials |
Metal-organic and hydride precursors |
Elemental or solid-source molecular beams |
| Typical strength |
High throughput and production scalability |
Research flexibility and atomic-scale interface control |
| Wafer capacity |
Often supports large or multiple wafers |
Frequently lower throughput |
| Common uses |
LEDs, lasers, GaN power devices, solar cells |
Quantum structures, research heterostructures, specialized devices |
The best process depends on material system, layer complexity, wafer diameter, production volume,
interface requirements, and available equipment.
MOCVD Applications
- LEDs: GaN, InGaN, and AlGaInP light-emitting structures
- Laser diodes: Quantum-well and heterostructure lasers
- Photodetectors: InGaAs/InP PIN and avalanche photodiodes
- HEMTs: AlGaN/GaN and InAlAs/InGaAs transistor structures
- Solar cells: GaAs and multi-junction III-V photovoltaic devices
- RF electronics: High-frequency and microwave semiconductor devices
- Power devices: GaN-based switching and high-voltage structures
- Photonics: Modulators, lasers, detectors, and optical integrated circuits
- Quantum structures: Quantum wells, dots, superlattices, and engineered barriers
- Infrared systems: Detectors, emitters, and optical communication components
MOCVD for InGaAs and InP Epitaxy
MOCVD is commonly used to grow InGaAs
epitaxial layers on InP
substrates. Lattice-matched In0.53Ga0.47As is especially important for
near-infrared photodetectors, optical communications, high-speed transistors, and sensing applications.
A typical InGaAs/InP structure may include:
- An n-type, p-type, or semi-insulating InP substrate
- An InP buffer layer
- An intrinsic or lightly doped InGaAs absorption layer
- InP window, cap, or contact layers
- Compositionally graded transition layers when required
Layer thickness, alloy composition, dopant species, carrier concentration, surface finish, and cap-layer
design are selected according to the intended photodiode, laser, transistor, or detector architecture.
MOCVD for GaN and Wide-Bandgap Devices
MOCVD is also the dominant epitaxial growth method for many GaN-based devices. GaN, InGaN, and AlGaN
layers may be grown on sapphire, SiC, silicon, or engineered templates for LEDs, laser diodes, RF
transistors, and power electronics.
GaN epitaxy presents challenges such as lattice mismatch, thermal-expansion mismatch, wafer bow, stress,
and defect management. Buffer layers, nucleation layers, graded structures, and strain-engineering
techniques are often used to improve film quality.
Rapid Thermal MOCVD
Rapid Thermal MOCVD refers to reactor designs or process approaches that heat and cool the
substrate rapidly. Fast thermal response can reduce cycle time, improve interface control, and limit the
time a wafer spends at elevated temperature.
Potential uses include:
Its practical benefits depend on reactor design, wafer size, temperature uniformity, material system,
and the thermal sensitivity of the complete layer structure.
How to Specify a Custom MOCVD Epi Wafer
Researchers requesting a custom MOCVD structure should provide as much of the following information as
possible:
- Substrate material, diameter, thickness, orientation, and conductivity type
- Layer sequence from the substrate to the top surface
- Thickness of each epitaxial layer
- Alloy composition and grading requirements
- Dopant species and target carrier concentration
- Desired cap, window, contact, or passivation layer
- Surface finish and backside requirements
- Quantity and acceptable characterization tolerances
UniversityWafer supplies III-V substrates and custom epitaxial structures for photonics, optoelectronics,
RF electronics, detectors, solar cells, and compound-semiconductor research.
Frequently Asked Questions About MOCVD
What is the main advantage of MOCVD?
Its key advantage is controlled deposition of multi-layer compound-semiconductor structures with scalable wafer processing. Composition, doping, and thickness can be adjusted for applications including LEDs, lasers, and photodetectors.
What are the main disadvantages of MOCVD?
The major limitations are expensive equipment, hazardous or reactive precursors, gas-handling requirements, process complexity, and the need to manage temperature and uniformity across wafers.
Is MOCVD the same as MOVPE?
In compound-semiconductor epitaxy, MOCVD and MOVPE generally describe the same metalorganic vapor-phase growth approach.
Which substrates are commonly used for MOCVD?
Common choices include GaAs, InP, sapphire, SiC, and selected silicon templates, depending on the epitaxial material system.
Related MOCVD and Epitaxy Resources
